Bagging line control
Product and bag size select the recipe and the line stops itself on completion. Reports total ingredient consumption, bags produced and kilos bagged per run.
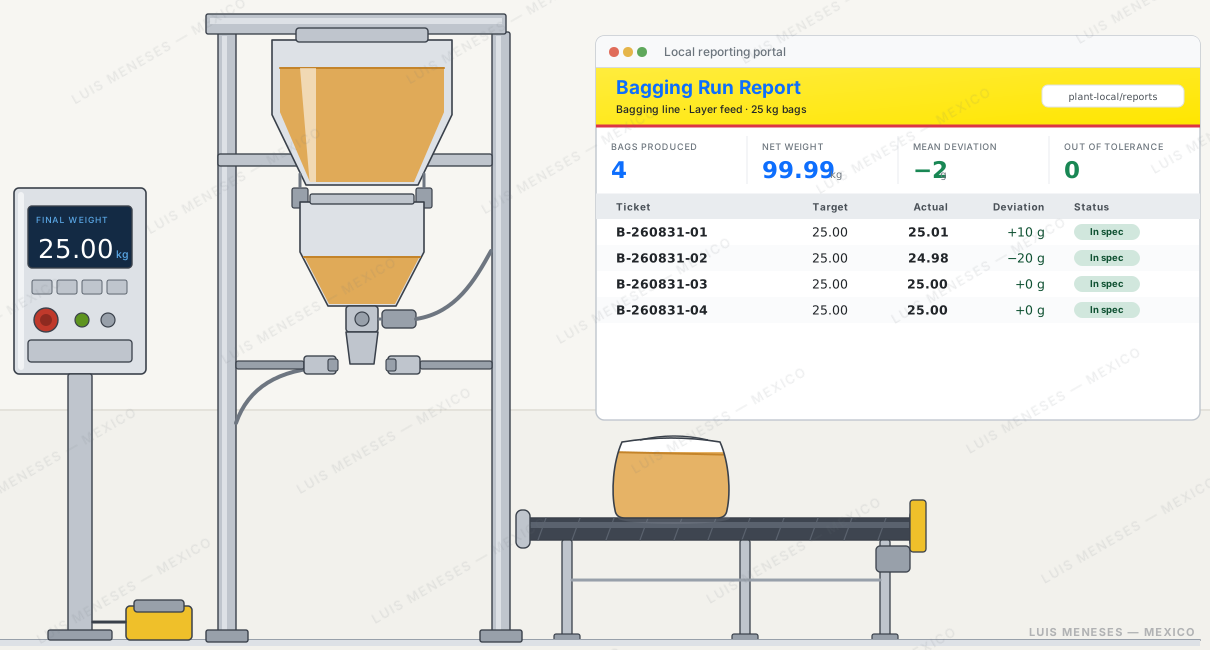
Bagging Run Report
| Ticket | Time | Target | Actual | Deviation | Status |
|---|---|---|---|---|---|
| B-260831-001 | 08:14:47 | 25.000 | 24.994 | −6 g | In spec |
| B-260831-002 | 08:15:34 | 25.000 | 24.994 | −6 g | In spec |
| B-260831-003 | 08:16:21 | 25.000 | 25.011 | +11 g | In spec |
| B-260831-004 | 08:17:08 | 25.000 | 24.997 | −3 g | In spec |
| B-260831-005 | 08:17:55 | 25.000 | 25.008 | +8 g | In spec |
| B-260831-006 | 08:18:42 | 25.000 | 24.981 | −19 g | In spec |
Product and target
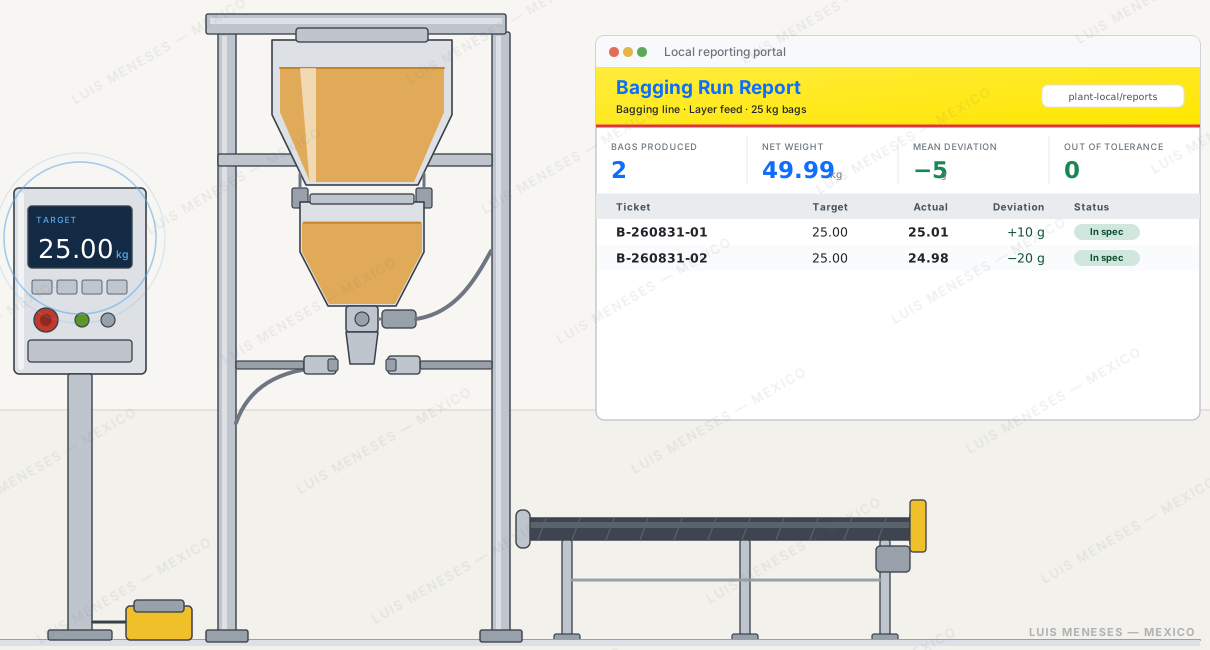
The operator picks the product and the bag size on the indicator. That choice is the recipe: it sets the target weight, the tolerance band and the preact value.
Bag placed, auto-tare
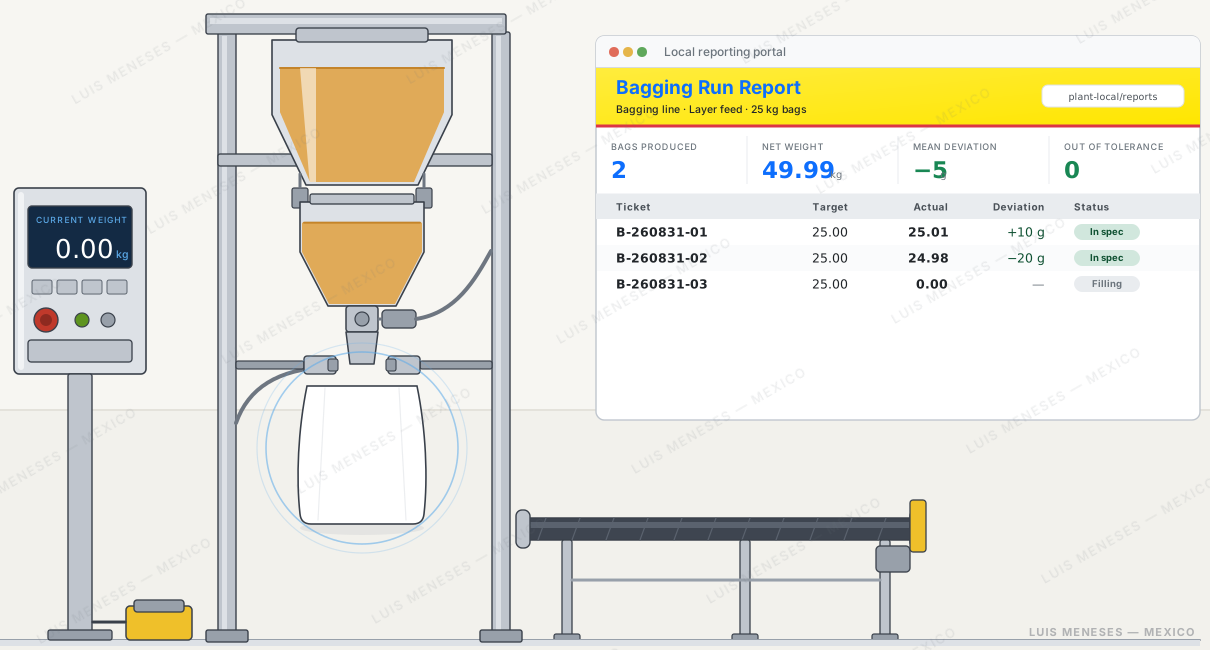
The empty bag goes on the spout and the pedal starts the cycle. The clamps hold it and the system tares itself, so the bag’s own weight never reaches the record.
Coarse fill
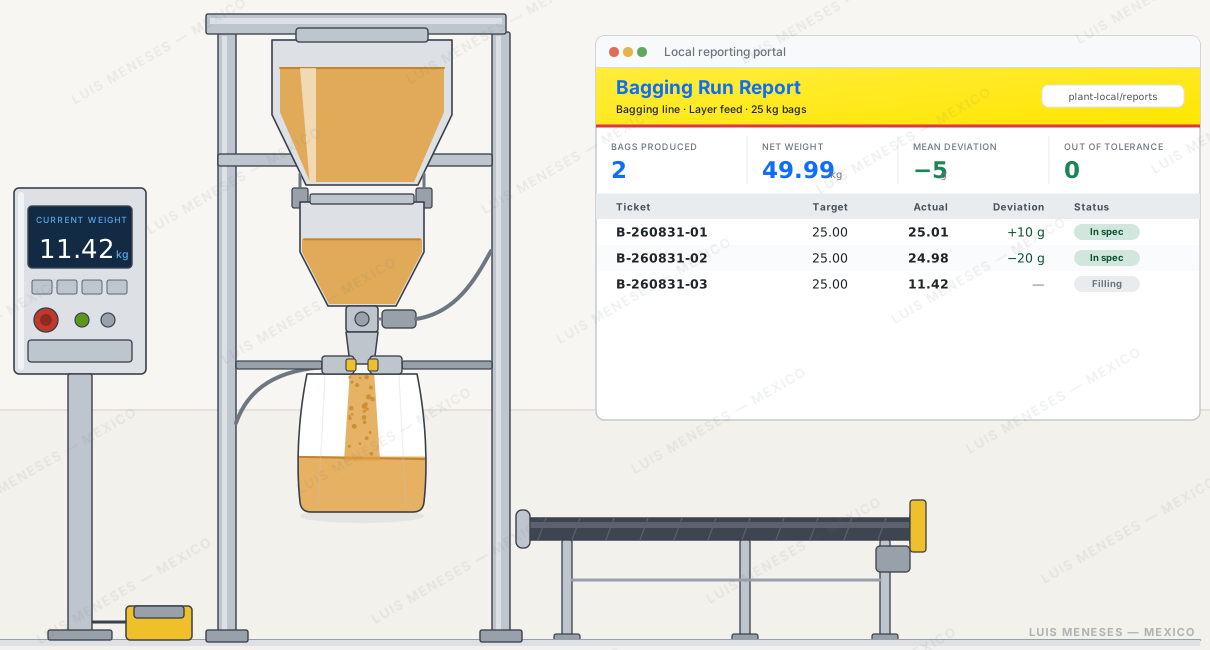
The main gate opens at full flow while the scale reads continuously. This stage puts in about ninety per cent of the target and is the part that decides throughput.
Fine fill and preact cut-off
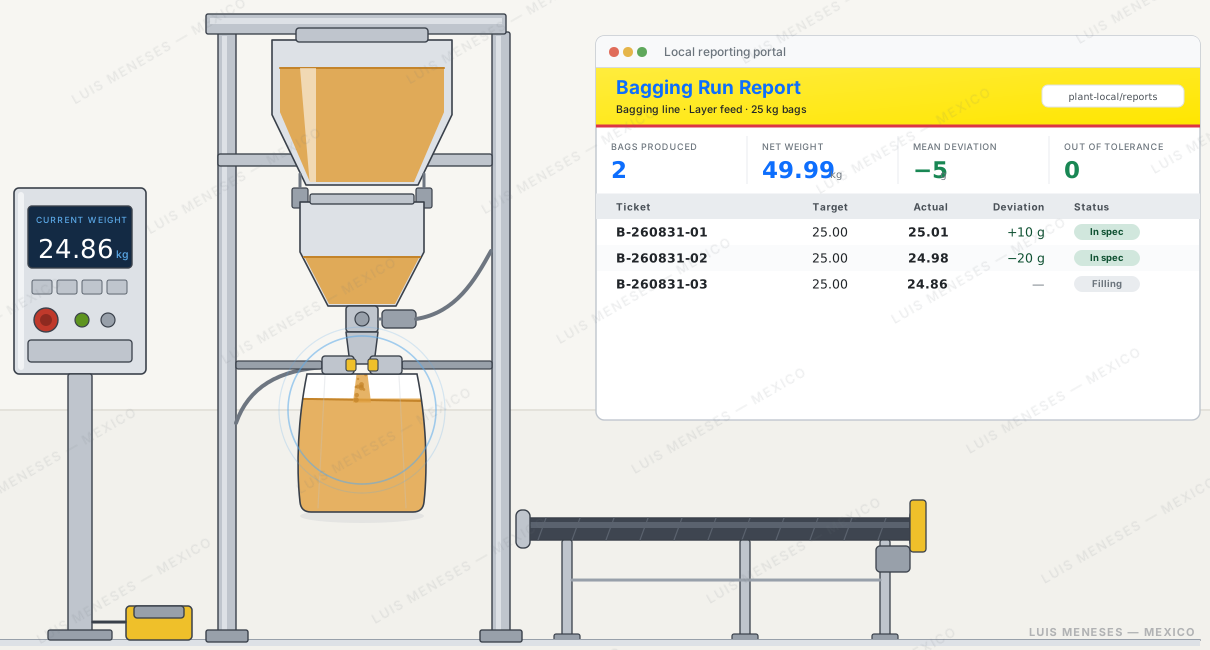
Flow drops to a trickle and the gate shuts before the target. The material already in flight finishes the weight — that in-flight compensation is what holds ±50 g, not the gate speed.
Released and logged
The clamps release the bag onto the conveyor. Ticket, actual weight and deviation go to the web platform, so every bag stays traceable by run, product and date.
The run, as a record
Where the cycle ends: not on the floor, but in the report the supervisor opens afterwards. Every bag, its target, its actual weight and its deviation — consumption and throughput fall out of that, they are not counted by hand.